Why Recycle Rare Earths?
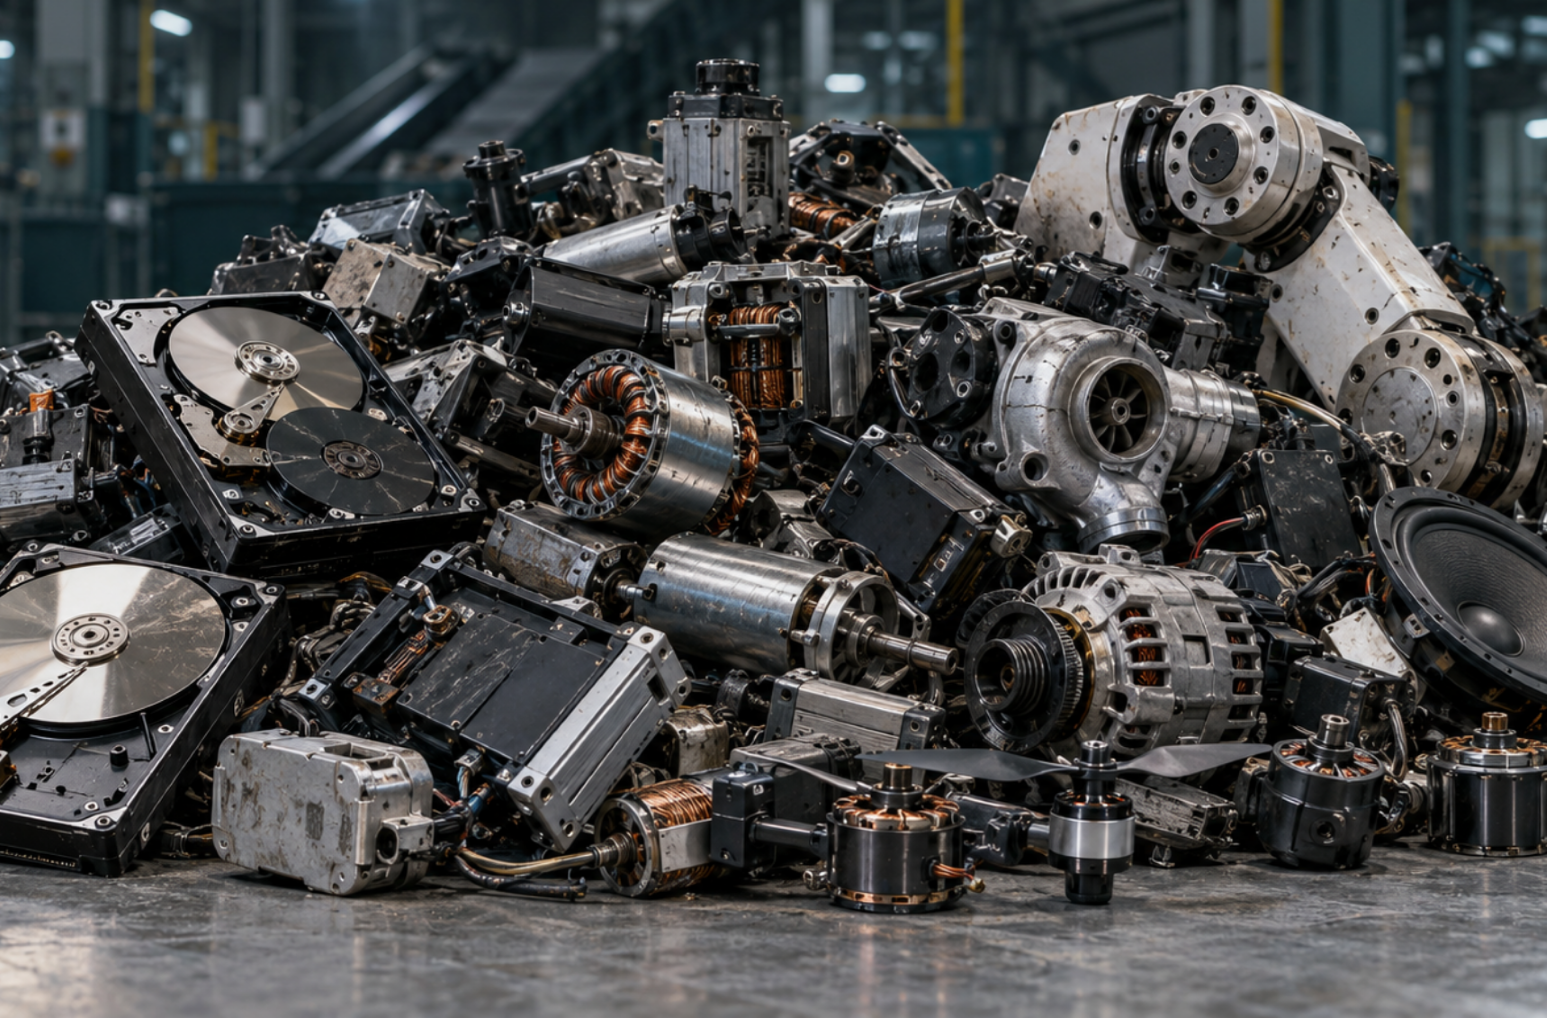
Rare earth permanent magnets are embedded in many of the technologies that keep modern economies moving. Their exceptional strength enables compact, lightweight and highly efficient motors, actuators, generators and other advanced components used across electric vehicles, e-bikes and e-scooters, robots, drones, wind turbines and medical devices. They are also found in hard disk drives, consumer electronics, and defense and aerospace systems.
When these products reach the end of their useful lives, the rare earth elements inside them do not lose their value. They remain concentrated within their permanent magnets and can become feedstock for new production, provided those magnets are identified, separated and directed to dedicated recovery infrastructure.
Demand is rising, but supply remains concentrated
Demand for rare earth elements is expected to grow significantly as the world relies more heavily on electrification, automation and AI. However, the global rare earth supply chain remains highly concentrated, with China accounting for more than 90% of refined rare earth production. This exposes manufacturers to geopolitical events, trade restrictions and other disruptions far beyond their operations.
New mines and processing facilities will form part of the solution, but they can take many years to reach production and require significant capital investment. By comparison, rare earth recovery infrastructure can be deployed far more rapidly, bringing additional supply online while longer-term mining projects are still being developed. Rare earth recovery can therefore complement mining by creating an alternate source of supply from materials already in circulation and adding processing capacity closer to manufacturers.
A valuable resource is being lost
Traditional recycling systems are generally designed to recover high-volume materials such as steel, aluminum and copper – not the rare earth magnets embedded within complex products.
Consequently, magnet-bearing components may be shredded and melted down with surrounding steel, preventing their rare earth content being recovered. Other products may be exported overseas within mixed scrap streams, taking their critical material value with them. Valuable rare earth resources are therefore frequently lost through conventional processing, export or downcycling rather than returned to manufacturing.
At the same time an abundant, readily available and above-ground resource is growing: End-of-life motors, actuators, hard disk drives, wind turbine generators, electronics and other products containing valuable rare earth permanent magnets. As increasing volumes of these technologies reach end of life, they will provide an increasingly important source of recoverable critical materials.
Creating a domestic destination for magnet-bearing materials
Dedicated critical material recovery provides a domestic destination for products and manufacturing scrap that might otherwise enter conventional waste streams.
For OEMs, scrapyards, electronics recyclers and IT asset disposition providers, identifying and separating magnet-bearing material creates a higher-value outlet and an additional potential revenue stream from scrap that has historically been overlooked. Keeping these materials within domestic and allied processing networks also improves traceability and strengthens regional supply chains.
Building a circular source of rare earth supply
At Cyclic Materials, we are building the infrastructure required to recover rare earth elements and reintroduce them into the manufacturing supply chain at commercial scale.
The rapid deployment of our first U.S. commercial-scale facility in Mesa, Arizona, demonstrates how quickly rare earth recovery capacity can be brought online compared with conventional mine development. We anticipate similarly rapid deployment of our next U.S. facility in McBee, South Carolina, as we continue expanding domestic rare earth recovery and processing capacity.
Through our rare earth recovery platform, magnet-bearing end-of-life products and manufacturing scrap are first processed to separate permanent magnets from surrounding steel and other materials. From there, their rare earth content can be extracted, refined and separated into high-purity oxides, and ultimately converted into rare earth metals for new permanent magnet production.
By connecting these stages, rare earth recovery transforms material that might otherwise be lost into a new source of supply for advanced manufacturing. With the ability to add capacity quickly and close to existing sources of feedstock, it can complement traditional mining, diversify processing capacity and keep critical materials in circulation.
